bagasse pulp
Learn More


 18:01
Bagasse paper plates are made by dispersing dried bagasse pulp sheets in water, forming the slurry into a plate shape on a vacuum mold, then hot-pressing the wet blank dry, trimming it and inspecting it. Pulp quality at step one, especially brightness, dirt count and beating degree, carries through to the finished plate.
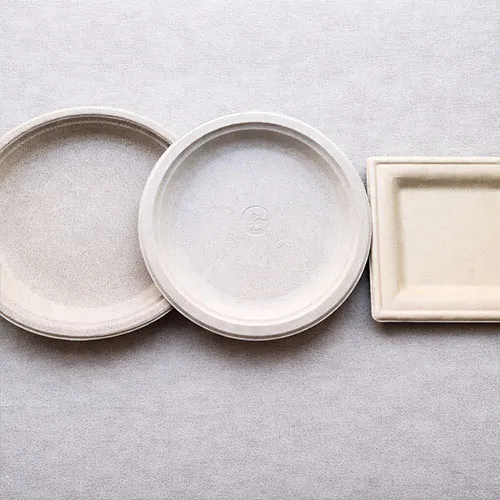
This route suits lines that form a wet blank and then dry it under heat and pressure. Lines built on other forming methods will differ in the middle steps, though the pulp checks at the start still apply.
| Parameter | Published value | Where it shows up |
| Brightness | >80% | Surface color of the finished plate |
| Dirt count, 0.3–5.0 mm² | <35 mm²/500 g | Dark specks on a white surface |
| Dirt count, >5.0 mm² | None | Large specks, which should not appear |
| Beating degree | 22 °SR | Drainage behavior on the forming mold |
| Moisture | <15% | Pulp arrives dry and must be fully dispersed |
| pH | 6.5–8.0 | Starting point for slurry pH before additives |
| Ash | <0.7% | Mineral content carried into the plate |
| Tensile index | >55 N·m/g | Fiber strength indicator, not plate strength |
| Viscosity | >550 cm³/g | Fiber integrity indicator |
| Fiber wet weight | >1.7 g | Fiber coarseness indicator |
| Sheet size | 700 × 800 mm | Feed size into the pulper |
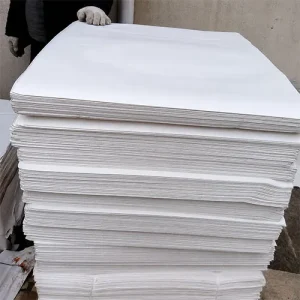
Check the incoming pulp against the datasheet. Confirm brightness, moisture, pH and sheet size on the lot certificate or test report, and look over a few sheets for visible specks. Done when the lot’s figures sit inside the published ranges and no sheet shows large dark specks. Dirt count itself needs a lab, so request the report instead of judging it by eye.
Disintegrate the sheets in water. Feed sheets into the pulper with water and run it until the fiber is dispersed. Water ratio and run time depend on your pulper, so take them from the equipment maker. Done when a small sample spread in a clear container shows no flakes or fiber lumps.
Bring the slurry to forming condition. Dilute to the concentration your forming mold needs and add any functional additives your formulation calls for. Check pH after the additives go in, because the pulp’s 6.5–8.0 range is the starting point and not the finished slurry. Done when two consecutive samples give the same concentration reading and pH holds steady.
Form the wet blank. A porous, mesh-faced mold takes in the slurry and vacuum pulls the water through, leaving a layer of fiber on the mesh. Done when the blank holds an even thickness and shows no holes or thin spots against a light.
Transfer the blank to the press tooling. Move the wet blank to the heated mold without tearing or folding it. Done when the blank sits flat in the cavity with the rim fully seated.
Hot-press and dry. Heated dies press the blank to shape and drive off water. Temperature, pressure and dwell time are specific to your machine, tooling and plate weight, so start from your equipment supplier’s figures and tune on trial pieces. Done when the plate demolds flat, has no damp center or blisters, and the weights of consecutive pieces stop changing.
Trim the edges. Cut flash from the rim and bring the plate to drawing size. Done when the rim is clean and the diameter sits inside your tolerance.
Inspect and record. Check color against a reference plate, count visible specks, test for warping, and run any leak or oil test your product claims need. Log the pulp lot against the production lot. Done when the sample passes your acceptance sheet and the lot traces back to its pulp batch.
| Bleached Bagasse Pulp | Unbleached Bagasse Pulp | |
| Brightness | >80% | 40–43% |
| Dirt count, 0.3–5.0 mm² | <35 mm²/500 g | <40 mm²/500 g |
| Dirt count, >5.0 mm² | None | None |
| Beating degree | 22 °SR | 18 °SR |
| Moisture | <15% | 14 ± 2% |
| pH | 6.5–8.0 | <8.0 |
Compared with marketplace tableware-pulp listings that name one grade and say nothing about how it is molded, a side-by-side like this at least lets you match the pulp to the surface finish you need. White plates point to the bleached grade, where specks show most. Natural-color plates can use the unbleached grade.For more information about the product, please contact us.
What pulp is used to make bagasse paper plates?
Sugarcane bagasse pulp. Sheeon supplies a bleached grade with brightness above 80% and an unbleached grade at 40–43%.
Why do the pulp sheets have to be disintegrated first?
Bleached Bagasse Pulp ships as dry sheets at 700 × 800 mm with moisture below 15%. The fiber has to be dispersed in water before it can be formed on a mold.
Can I test the pulp before a bulk order?
Sheeon lists sample development and technical support among its services. Ask for a sample of the grade you plan to use and run steps 2 to 6 on one lot.
Bagasse pulp is fiber made from sugarcane bagasse, the residue left after juice extraction. Sheeon offers a bleached grade with brightness above 80% and an unbleached grade at 40–43%. Choose by brightness target, cleanliness limits and strength data, then verify certificates and test samples before committing to volume. What sugarcane bagasse pulp is Sugarcane bagasse […]

Bamboo paper is made from bamboo fiber; tree paper is made from wood pulp. Neither wins outright, because performance depends on the pulp grade. Sheeon’s bleached bamboo pulp publishes brightness near 85% and fiber length above 1.7 mm, which gives buyers fixed numbers to test any virgin wood pulp against. Where the fibers come from […]